English
 中文简体
Call us
+86-13814563863

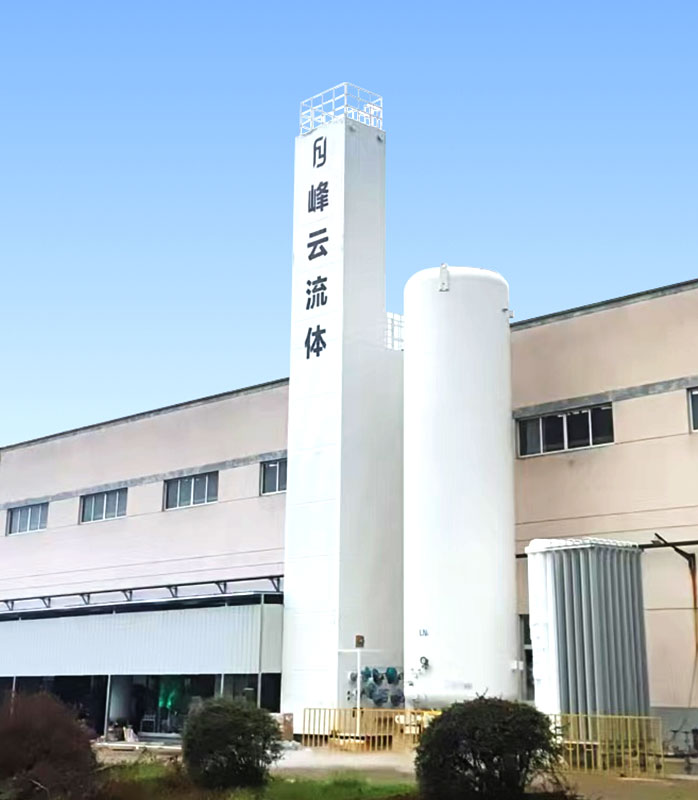

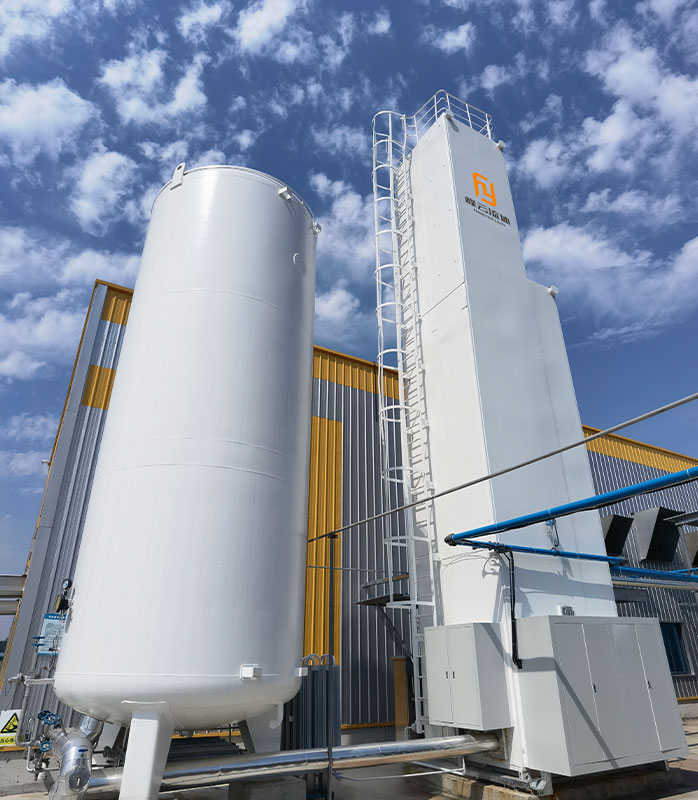
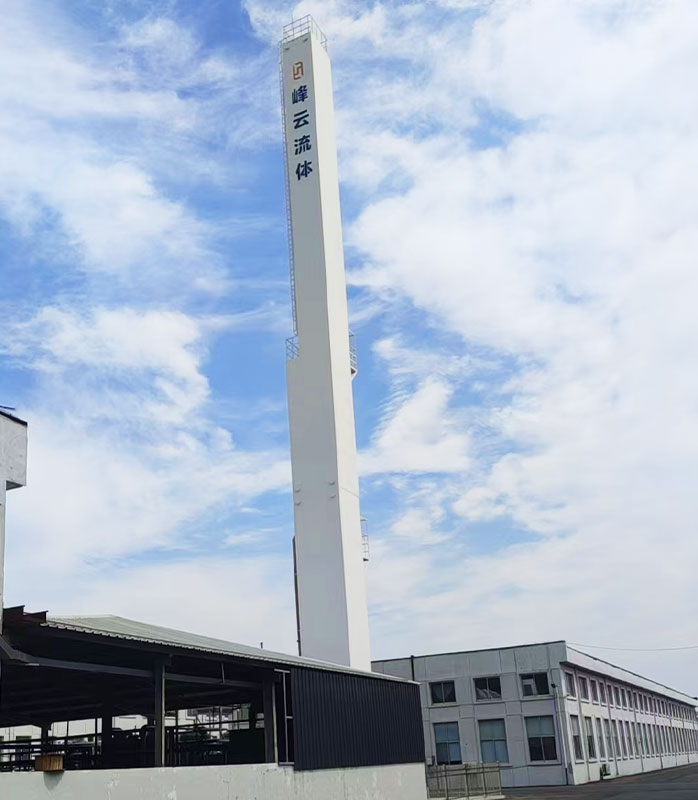
A Cryogenic Air Separation Plant(also known as Air Separation Unit, ASU) is an industrial gas production system that utilizes low-temperature distillation technology to separate and purify oxygen, nitrogen, and other components from ambient air.
Our Solutions
Leveraging advanced cryogenic separation technology, Fengyun Fluid provides comprehensive, large-scale industrial gas production solutions. Our end-to-end services encompass system design, equipment integration, installation and commissioning, intelligent control systems, and long-term operation and maintenance services.
Core Process
Through core process stages—including air compression, molecular sieve purification, low-temperature heat exchange, expansion refrigeration, and cryogenic distillation—we ensure a continuous and stable supply of high-purity industrial gases.
Suzhou Fengyun Fluid Technology Co., Ltd. is famous China Cryogenic Air Separation Plant Manufacturers and custom industrial cryogenic ASU plant suppliers, specializes in the design, manufacturing, delivery, and operation of cryogenic air separation systems for industrial oxygen, nitrogen, and argon.
Backed by a team of 86 engineers and technical specialists, the company's capabilities span air compression and separation station planning, air compression systems and air separation equipment sales and leasing, on-site gas generation, and outsourced technical services. Leveraging an IoT-enabled platform, Fengyun delivers smart gas supply solutions tailored to customer operations.
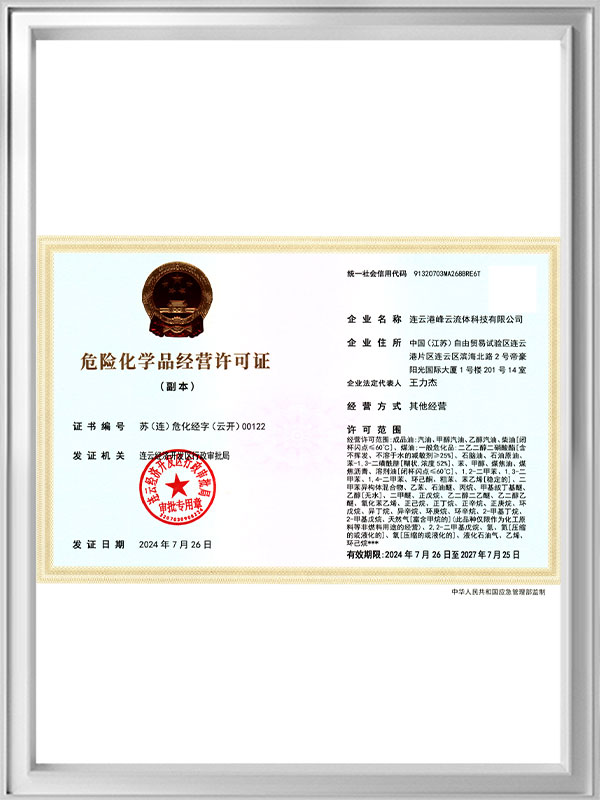
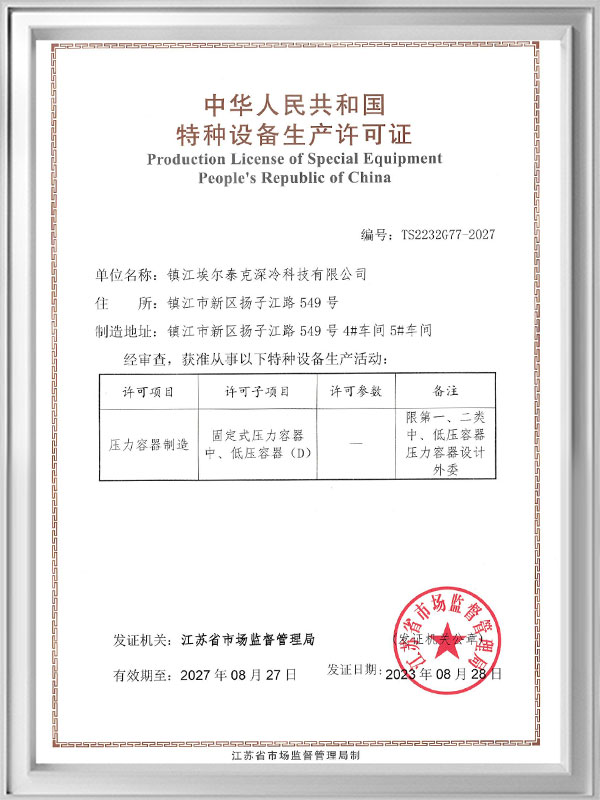
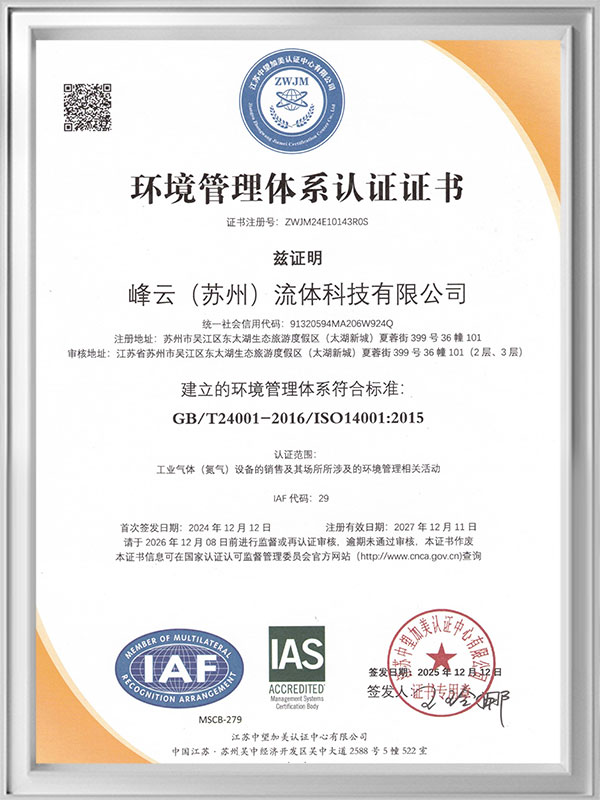
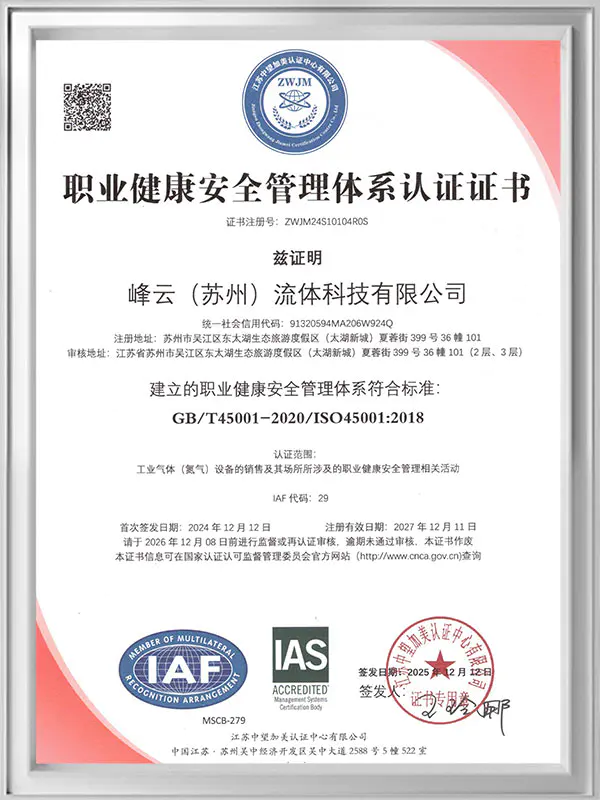
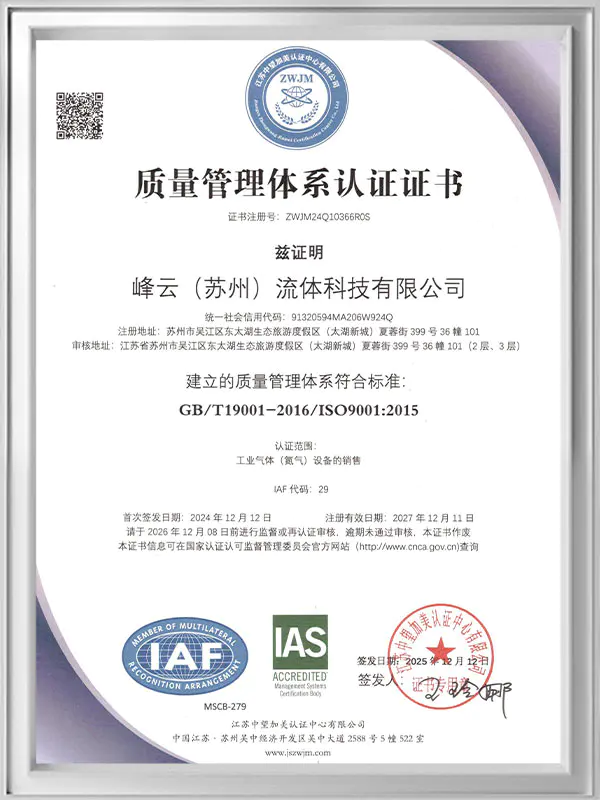
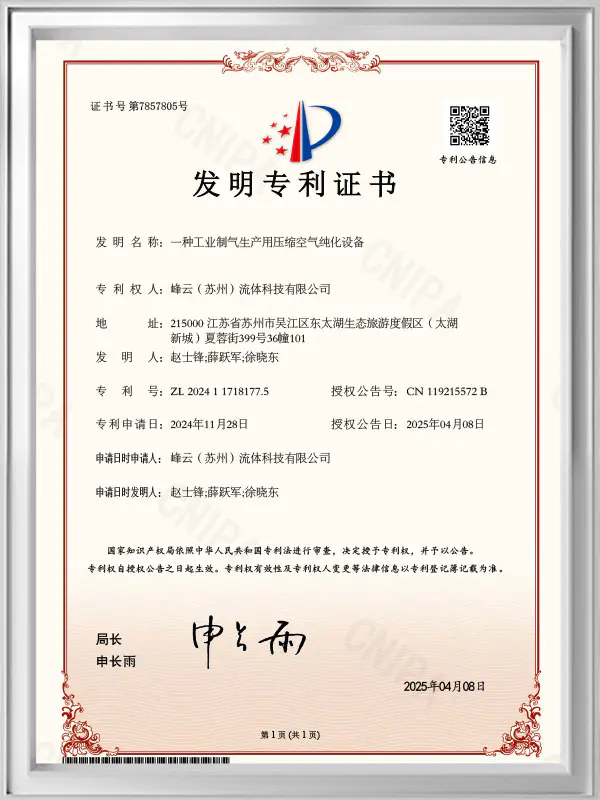
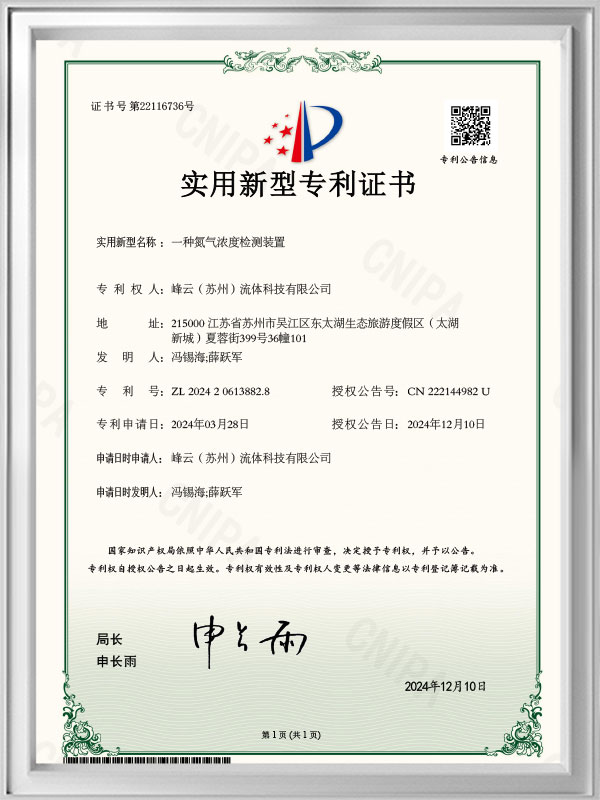
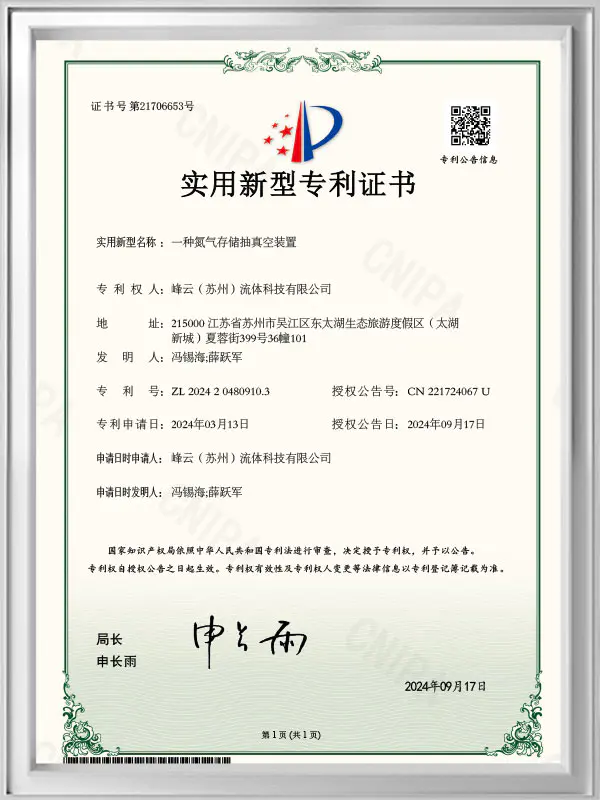
In large-scale industrial gas production, the Cryogenic Distillation Column (also referred to as the fractionation tower or distillation column) serves as the core thermodynamic separation unit. Oper...
READ MORENitrogen is an indispensable utility across modern manufacturing, chemical synthesis, metallurgy, and electronics fabrication. While smaller or medium-scale demands are frequently satisfied by Pressu...
READ MOREIndustrial gas supply is a critical backbone for modern manufacturing, energy, and chemical infrastructure. Among the various gas separation methods available today, the Cryogenic Air Separation Plan...
READ MORETraditional air separation plant operation relies heavily on on-site personnel, with slow fault response and high inspection costs. Fengyun Fluid integrates IoT technology into products and services, ...
READ MORESuzhou Fengyun Fluid Technology Co., Ltd. is a premier engineering manufacturer and global solution provider specializing in custom cryogenic air separation systems. As leading China cryogenic air separation plant manufacturers and premier China industrial cryogenic ASU plant suppliers, we design, fabricate, erect, and commission complete air separation facilities that produce high-purity gaseous and liquid oxygen, nitrogen, and argon. Supported by an experienced engineering staff of 86 technical specialists, our custom plants serve demanding sectors including steel metallurgy, chemical synthesis, semiconductor packaging, glass manufacturing, and regional industrial gas supply networks.
From our advanced cryogenic air separation plant factory, we manufacture essential cryogenic process assets—such as multi-stage main air compressors, pre-cooling air chillers, temperature swing adsorption molecular sieve purifiers, brazed aluminum plate-fin heat exchangers, high-efficiency distillation cold boxes, and expansion refrigeration turbines. By maintaining direct manufacturing oversight across every stage of fabrication, our custom cryogenic air separation plant factory guarantees superior thermodynamic efficiency, minimal specific power consumption, strict pressure vessel safety compliance, and long-term mechanical reliability for industrial facility owners worldwide.
In contrast to intermediate equipment vendors or non-manufacturing engineering brokers, Suzhou Fengyun Fluid Technology Co., Ltd. operates a comprehensive production center equipped for heavy plate rolling, precision CNC tube sheet machining, automated orbital welding, and cryogenic cold box column fitting. Partnering directly with experienced custom cryogenic air separation plant manufacturers allows plant operators, project managers, and EPC contractors to eliminate unnecessary procurement markups while securing specialized technical customization from the initial process flow simulation to final site acceptance testing.
Our air separation systems are engineered to replace costly bulk liquid transport, merchant gas contracts, and vulnerable delivery logistics with reliable, on-site industrial gas production. By converting atmospheric air into precise volumes of high-purity oxygen, nitrogen, and argon directly at your facility boundary, our cryogenic plants deliver predictable utility costs, robust supply security, and reduced total cost of ownership across decades of operation.
We directly fabricate pressure vessels, purification beds, and distillation column internals in-house. Strict non-destructive testing (NDT), X-ray weld inspection, and helium mass spectrometer leak detection ensure leak-free vacuum insulation and long-term structural integrity.
Our thermodynamic process modeling integrates low-pressure double-column distillation, high-efficiency liquid pump internal compression cycles, and expansion turbine refrigeration recovery to achieve industry-leading specific power efficiency per unit of gas generated.
Integrated DCS and PLC control architecture pairs seamlessly with our proprietary cloud-based IoT platform, providing automated variable load adaptation, live purity analysis, preventive maintenance alerts, and 24/7 remote operational support.
To address distinct gas product requirements, site footings, and power utility constraints, Suzhou Fengyun Fluid Technology presents a categorized suite of air separation plant series. Each series represents a configurable engineering architecture tailored to specific capacity scales and purity targets.
Designed for continuous, large-volume production of high-purity gaseous nitrogen (GAN) and liquid nitrogen (LIN) via low-temperature liquefaction and fractional separation. Ideal for inerting, reactor blanketing, wafer fabrication, and metallurgical heat treatment.
Configured for direct pipeline delivery to chemical manufacturing complexes, petrochemical refineries, and microelectronics plants requiring steady baseline nitrogen flow with strict O2 impurity limits down to less than 1 ppm.
Incorporates high-pressure recycle compressor loops and dual cryogenic expansion turbines to maximize liquid yields. Supplies bulk liquid nitrogen storage tanks for regional distributor filling and food cryo-freezing hubs.
Engineered for high-volume gaseous oxygen (GOX) and liquid oxygen (LOX) separation. We offer both internal compression (liquid oxygen pump with high-pressure main heat exchanger) and external gaseous oxygen compression system designs.
Utilizes submerged cryogenic pumps inside the cold box to elevate liquid oxygen to designated discharge pressures before vaporizing it against booster feed air streams. This modern design eliminates gaseous oxygen compressors, significantly improving operational safety and overall system availability in steelworks.
Produces continuous medical grade oxygen for healthcare facility pipeline systems while simultaneously filling liquid oxygen reserve tanks and high-pressure gas cylinder racks for local industry.
Advanced air separation plants featuring full argon recovery without hydrogen addition, capturing oxygen, nitrogen, and high-purity refined argon (LAR) in a unified cryogenic process.
Configured with secondary crude argon columns and packed deoxo distillation systems to supply multi-client industrial parks with gaseous oxygen, gaseous nitrogen, and liquid argon for stainless steel welding and silicon crystal growing.
Pre-assembled and factory-tested on rigid structural skid frames for rapid installation in remote mining camps, island sites, or overseas industrial projects requiring short installation cycles.
The following practical table provides technical comparisons across our main cryogenic air separation plant categories, detailing output gas purity, capacity scale, working pressure ratings, material choices, and control integration:
| Plant Configuration | Primary Target Gas Output | Achievable Purity Limit | Standard Flow Capacity | Pipeline Discharge Pressure | Key Structural Materials | Automation & PLC Interface |
| High-Purity Nitrogen ASU | Gaseous N2 / Liquid N2 | 99.9999% (O2 ≤ 1 ppm) | 1,000 to 40,000 Nm³/h | 0.5 - 1.6 MPa | Aluminum 6061-T6 / Stainless Steel 304L | Siemens S7-1500 PLC + WinCC HMI / DCS |
| Internal Compression Oxygen ASU | Gaseous O2 / Liquid O2 | 99.6% - 99.8% | 2,000 to 50,000 Nm³/h | 0.2 - 3.5 MPa (liquid pumped) | Stainless Steel 316L / Vacuum Perlite Casing | Redundant DCS + Safety ESD Interlock |
| Full Fractionation Tri-Gas ASU | O2 + N2 + Liquid Argon | O2 99.6%, N2 5N, Ar 99.999% | 10,000 to 60,000 Nm³/h | Multi-stream pressure manifold | Structured Al Packing / Cryogenic Valve Assemblies | Centralized Plant DCS + IoT Remote Cloud |
| Full Merchant Liquefaction Plant | LOX + LIN + LAR (100% Liquid) | Ultra-High Pure Liquid Grade | 100 to 1,000 tons/day liquid | 0.2 - 0.8 MPa storage filling | SS304 Inner Tank / Outer Carbon Steel Shell | Automated Bulk Tank Farm Metering System |
| Modular Skid-Mounted ASU | Gaseous O2 or N2 Skid | 99.5% O2 / 99.99% N2 | 300 to 2,500 Nm³/h | 0.6 - 1.0 MPa | Structural Carbon Steel Base Frame / SS Skid | Integrated Touchscreen HMI + Remote Gateway |
Cryogenic air separation represents the most cost-efficient and reliable technical route for high-volume, multi-gas industrial production. Our customized plant configurations address the specialized operational requirements of major process industries:
Delivers massive oxygen streams for oxygen enrichment in ironmaking blast furnaces and steel converter blowing, combined with high-purity argon for secondary ladle metallurgy.
Supplies oxygen for coal gasification and partial oxidation reactors while providing constant nitrogen streams for chemical tank blanketing, catalyst regeneration, and flare stack purging.
Provides ultra-pure 6N nitrogen gas for silicon wafer deposition chambers, cleanroom purging, and inert atmosphere carrier gas applications with zero moisture contamination.
Utilizes pure gaseous nitrogen for liquefied natural gas (LNG) pipe cooldown, line purging, and calorific value adjustment prior to grid distribution.
To assist our technical team in formulating a comprehensive engineering proposal, calculating heat balances, and selecting optimal compressor and expander frames, buyers should provide the following baseline project inputs:
Suzhou Fengyun Fluid Technology Co., Ltd. provides full EPCM (Engineering, Procurement, Construction Management) project execution. Our team guides project managers from site layout design and civil foundation preparation through cold box vertical lifting, pipe manifold welding, cold commissioning, and performance guarantee verification.
Our technical field specialists direct cold box vertical erection, column precision alignment, interconnection piping, and perlite insulation filling, ensuring zero thermal leaks and optimal structural stability.
Factory Acceptance Testing (FAT) validates vessel hydro-testing, valve stroke actuation, and PLC panel logic. Site Acceptance Testing (SAT) certifies plant cooldown timing, gas purity achievement, flow capacity, and emergency shutoff loops.
We offer comprehensive maintenance agreements, including spare parts stocking, compressor overhauls, molecular sieve bed replacement, and 24/7 cloud IoT diagnostics to ensure continuous, uninterrupted gas production uptime.
Unlike equipment traders or third-party engineering intermediaries, Suzhou Fengyun Fluid Technology operates a dedicated equipment manufacturing facility backed by an 86-person engineering team. Recognized among top China industrial cryogenic ASU plant suppliers, we design and build core distillation columns, molecular sieve beds, and heat exchange systems in-house. This direct engineering oversight yields significant CAPEX savings, guaranteed compliance with international pressure vessel codes, superior thermodynamic energy performance, and direct OEM field service.
Internal compression utilizes submerged cryogenic liquid oxygen pumps inside the insulated cold box to raise liquid oxygen pressure prior to vaporizing it against high-pressure air streams in main plate-fin heat exchangers. This completely eliminates high-pressure gaseous oxygen compressors outside the cold box, removing the mechanical friction and ignition risks associated with high-pressure gaseous oxygen machinery, while reducing compressor maintenance costs.
Our automated DCS and PLC control architectures incorporate dynamic load-following algorithms that interface with variable frequency drive (VFD) air compressors and adjustable guide vanes on expansion turbines. When downstream factory gas consumption drops, the system automatically adjusts feed air flow rate and column reflux ratios in real time, maintaining target product purity while lowering electricity consumption.
For modular or containerized skid-mounted ASU units, site installation, piping connections, and cold commissioning typically take 3 to 6 weeks. For large-scale custom cryogenic plants erected on site (10,000+ Nm³/h capacity), civil work supervision, cold box erection, insulation filling, and system integration take approximately 3 to 5 months, followed by a 24 to 48-hour plant cooldown period prior to final Site Acceptance Testing (SAT).
Our IoT platform collects live telemetry parameters—including temperature gradients, pressure drop across molecular sieves, vibration metrics on turbo expanders, and product purity levels. Predictive algorithms analyze these data streams to detect minor performance deviations before they cause unscheduled downtime. Plant engineers receive automated maintenance alerts, and our technical center can provide remote process tuning and operational diagnostics 24 hours a day.
edmondwong01@gmail.com
+86-13814563863
Room 101, Building 36, No. 399 Xiarong Street, Wujiang District, Suzhou,Jiangsu, China
* If you are interested, please leave a message on the left.
As professional cuztomized cryogenic air separation plant factory, Fengyun has built an IoT-enabled smart O&M platform that connects directly to your on-site equipment. It delivers proactive alerts, remote diagnostics and energy efficiency analytics, while dispatching local service teams for rapid response to keep your production running without interruption.
Quick Links