English
 中文简体
Call us
+86-13814563863

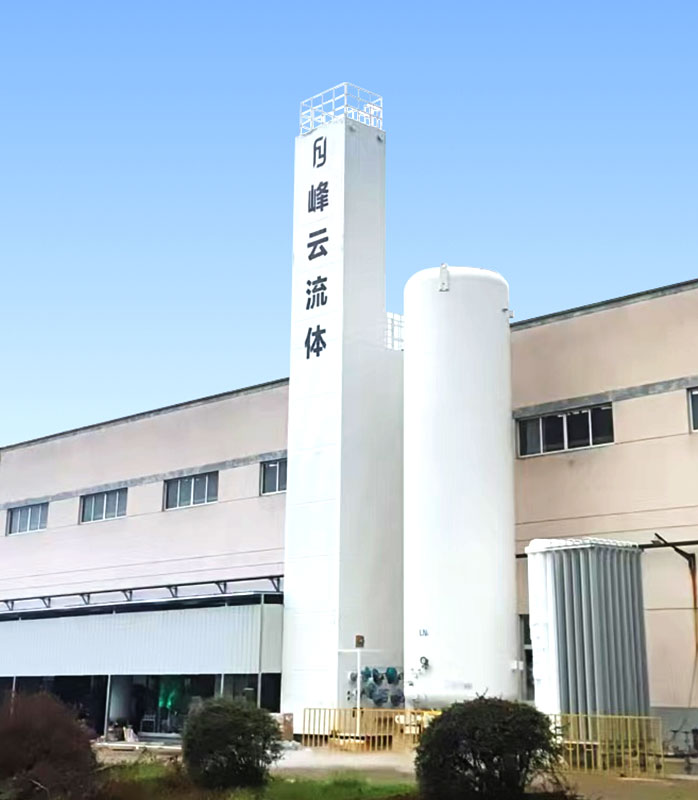

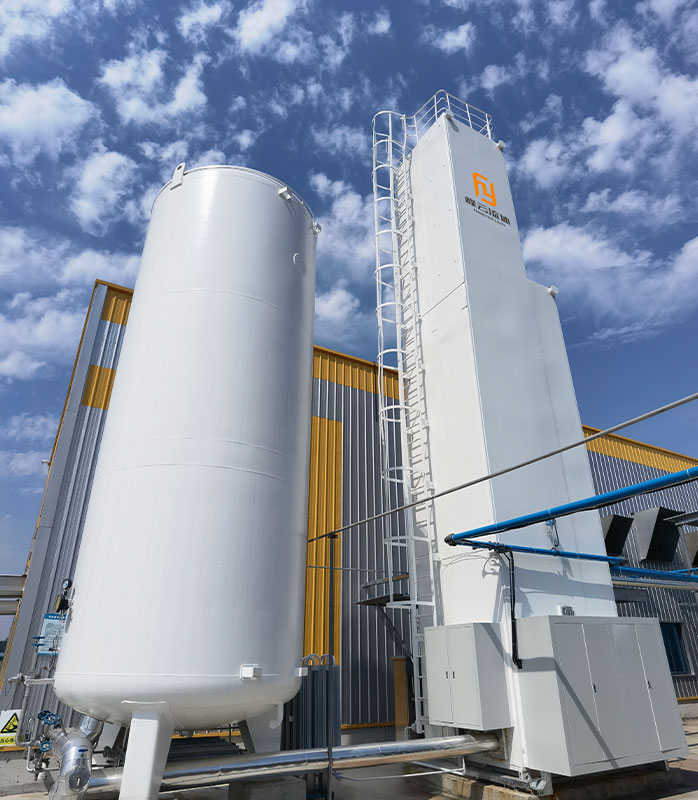
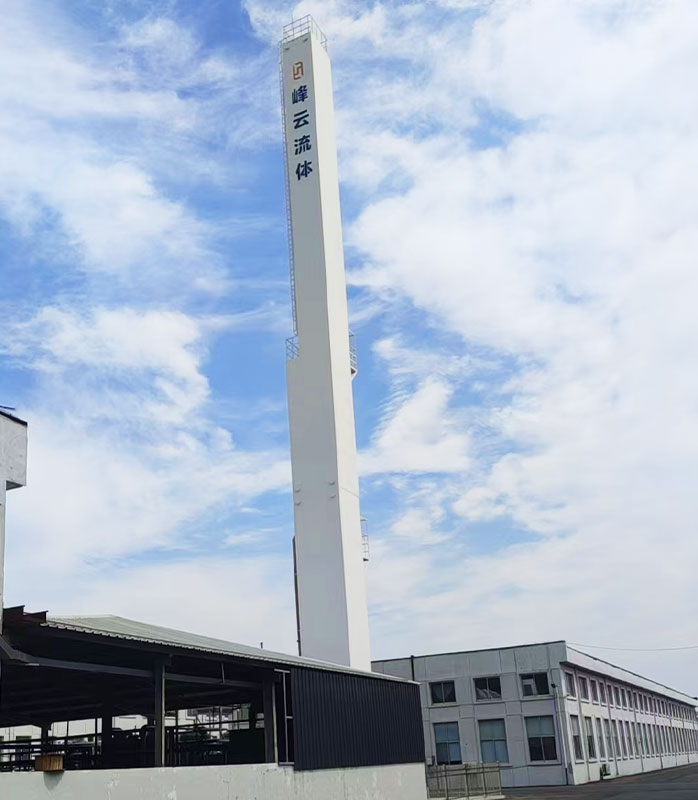
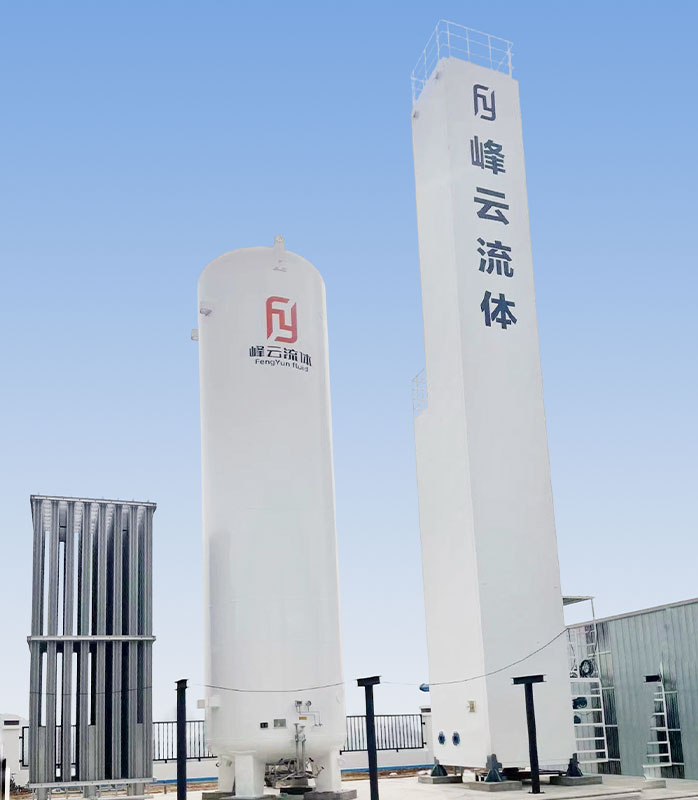
Suzhou Fengyun Fluid Technology Co., Ltd. is famous China Cryogenic ASU System Solutions Provider and customized industrial cryogenic ASU solutions, specializes in the design, manufacturing, delivery, and operation of cryogenic air separation systems for industrial oxygen, nitrogen, and argon.
Backed by a team of 86 engineers and technical specialists, the company's capabilities span air compression and separation station planning, air compression systems and air separation equipment sales and leasing, on-site gas generation, and outsourced technical services. Leveraging an IoT-enabled platform, Fengyun delivers smart gas supply solutions tailored to customer operations.
In large-scale industrial gas production, the Cryogenic Distillation Column (also referred to as the fractionation tower or distillation column) serves as the core thermodynamic separation unit. Oper...
READ MORENitrogen is an indispensable utility across modern manufacturing, chemical synthesis, metallurgy, and electronics fabrication. While smaller or medium-scale demands are frequently satisfied by Pressu...
READ MOREIndustrial gas supply is a critical backbone for modern manufacturing, energy, and chemical infrastructure. Among the various gas separation methods available today, the Cryogenic Air Separation Plan...
READ MORETraditional air separation plant operation relies heavily on on-site personnel, with slow fault response and high inspection costs. Fengyun Fluid integrates IoT technology into products and services, ...
READ MOREAs a specialized manufacturer and cryogenic ASU system solutions provider, Suzhou Fengyun Fluid Technology Co., Ltd. delivers custom engineered, turnkey cryogenic air separation plants and auxiliary equipment for global industrial gas consumers. Backed by a dedicated engineering team of 86 technical specialists, we design, manufacture, integrate, and deploy complete cryogenic air separation units (ASUs) that convert ambient air into high-purity gaseous and liquid oxygen, nitrogen, and argon.
Our manufacturing philosophy centers on long-term mechanical reliability, superior thermodynamic efficiency, and full lifecycle engineering support. From initial gas consumption profile modeling and compressor station planning to cold box fabrication, molecular sieve purifier assembly, and IoT-enabled remote operations, we supply complete industrial gas generation infrastructures tailored specifically to metallurgical plants, chemical synthesis complexes, semiconductor fabrication facilities, and regional gas distributors.
At Suzhou Fengyun Fluid Technology Co., Ltd., we maintain total control over the cryogenic equipment manufacturing lifecycle. Rather than acting as a third-party equipment broker, our in-house engineering and production facility manufactures the core process assets that dictate ASU stability, power consumption, and gas purity. By controlling the fabrication of distillation columns, heat exchanger integration, and skid mounted purification systems, we lower total cost of ownership (TCO) for project managers and plant engineers while ensuring strict alignment with international pressure vessel and quality codes.
Our industrial cryogenic ASU solutions are developed to eliminate the logistical vulnerabilities, recurring delivery costs, and evaporation losses inherent in bulk liquid transport and cylinder gas purchasing. By generating industrial gases on-site at exact pressure and purity parameters, operating facilities achieve predictable utility billing and continuous operational autonomy.
Every cryogenic vessel, aluminum plate-fin heat exchanger, and structural cold box frame undergoes rigorous non-destructive testing (NDT), helium leak testing, and hydraulic/pneumatic pressure verification to ensure zero vacuum degradation over decades of service.
Our thermodynamic process design utilizes advanced internal compression cycles and high-efficiency turbo expanders, minimizing specific power consumption (kWh per Nm3 of gas generated) and maximizing energy recovery across cold box circuits.
Integrated cloud-connected control systems continuously track temperature, pressure, flow rate, and purity parameters in real time, delivering automated fault warnings, predictive maintenance scheduling, and remote operating optimization.
To accommodate diverse operational scales, installation footprints, and multi-gas supply requirements, our product portfolio is divided into two main categories: Turnkey Cryogenic Air Separation Plants and Modular Cryogenic Technology & Auxiliary Equipment. Each series represents a fully selectable, configurable engineering solution designed for targeted industrial duties.
Designed for medium- to large-scale continuous gas supply, our complete cryogenic air separation plants utilize fractional distillation at temperatures down to -196°C to isolate atmospheric gases with ultra-high purity.
The Cryogenic Nitrogen Generation System isolates high-purity nitrogen gas and liquid nitrogen directly from air feed through low-temperature liquefaction and distillation. It provides large-scale, cost-effective nitrogen generation for inerting, purging, chemical blanketing, and electronics manufacturing.
Utilizing multi-stage distillation column structures and precise thermal management, our Cryogenic Oxygen Generation Systems yield industrial and medical grade gaseous and liquid oxygen. Designed for heavy metallurgy, glass melting furnaces, pulp bleaching, and wastewater oxidation.
An integrated dual-production ASU system configured to simultaneously extract pure gaseous nitrogen, oxygen, and crude or refined argon from a unified air processing cold box. Ideal for industrial parks, large steelworks, and multi-discipline chemical production hubs requiring flexible gas ratios.
For system revamps, capacity expansions, or custom module integration, Suzhou Fengyun Fluid Technology manufactures standalone core cryogenic machinery engineered to exact industrial duty cycles.
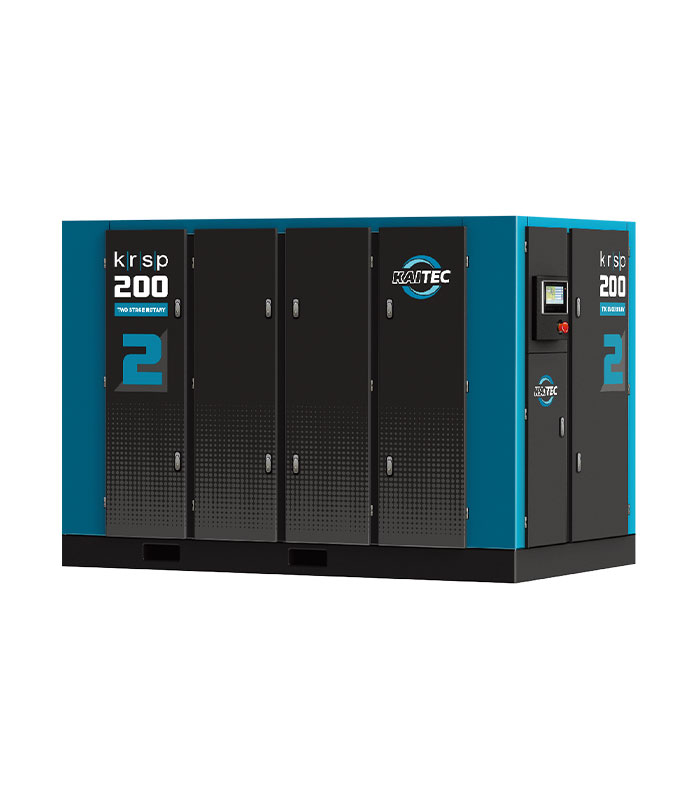
Model range KRSP-18-8 to KRSP2-455-10 heavy-duty air compressors serve as the main motive power source for the ASU. They compress ambient air to elevated working pressures with high volumetric efficiency, providing continuous, stable feed air to pre-cooling and purification units.
Engineered to protect downstream cryogenic heat exchangers and distillation columns, our dual-bed molecular sieve purifiers remove moisture (H2O), carbon dioxide (CO2), and trace hydrocarbons (acetylene, heavy hydrocarbons) from feed air via temperature swing adsorption (TSA) or pressure swing adsorption (PSA).
The technological heart of cryogenic air separation. Housing upper and lower column sections, main condenser-reboilers, and structured aluminum packing inside a fully insulated steel cold box vessel, this column achieves high mass-transfer efficiency for liquid-vapor phase separation.
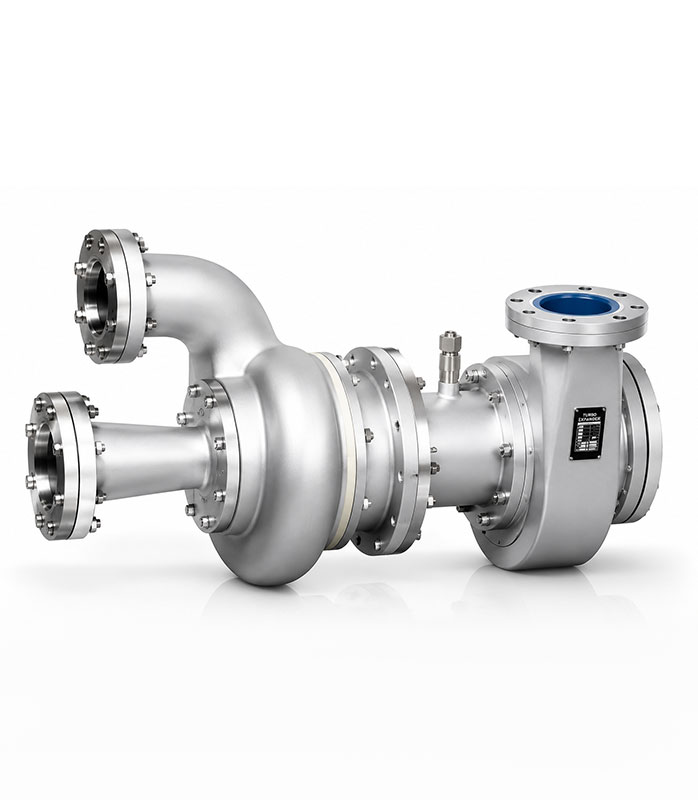
The primary refrigeration engine of the ASU system. By expanding high-pressure process gas through a precision-machined radial expansion turbine wheel, it produces the refrigeration duty necessary to compensate for heat leak and achieve air liquefaction.
The following technical summary details the operating parameters, output gas purity levels, capacity thresholds, and structural materials across our standard cryogenic system configurations:
| System Configuration | Primary Target Gas | Achievable Purity | Standard Capacity Range | Operating Pressure | Core Materials | Automation Integration |
|---|---|---|---|---|---|---|
| Cryogenic Nitrogen Generator | Gaseous N2 / Liquid N2 | 99.99% - 99.9999% (O2 ≤ 1 ppm) | 500 to 35,000 Nm³/h | 0.5 - 1.2 MPa (customizable) | SS304L / Aluminum Alloy 6061-T6 | Siemens S7 PLC / DCS Smart IoT |
| Cryogenic Oxygen Generator | Gaseous O2 / Liquid O2 | 95.0% - 99.8% | 1,000 to 50,000 Nm³/h | 0.15 - 3.0 MPa (pumped liquid/gas) | SS316L / Brazed Aluminum Heat Exchanger | Full DCS / Redundant Instrument Loop |
| Combined N2/O2/Ar ASU | O2 + N2 + Liquid Argon | N2 99.999%, O2 99.6%, Ar 99.999% | 3,000 to 60,000 Nm³/h | 0.2 - 2.5 MPa Multi-pressure | Cryogenic Grade Austenitic Steel / Al-Pack | Centralized Control Room + IoT Cloud |
| KRSP Air Compressor Station | Compressed Ambient Air | Cleaned, Oil-free compressed feed | 18 kW to 455 kW per compressor unit | 0.8 - 1.0 MPa outlet pressure | Heavy-duty cast iron / SS impellers | Integrated VFD / Group control protocol |
| Molecular Sieve Purifier Skid | Purified Process Air | H2O ≤ 1 ppm, CO2 ≤ 1 ppm | Matched to ASU flow rate | 0.6 - 1.0 MPa working rating | Pressure Vessel Steel Q345R / 13X Sieve | Automated Pneumatic Valve Switching PLC |
Cryogenic air separation remains the industry gold standard for large-volume industrial gas generation due to its unmatched purity limits, economy of scale, and capability to produce liquid co-products for strategic reserve storage. We tailor plant architecture based on industry-specific operating demands:
Requires continuous ultra-pure nitrogen (99.9999% purity) with non-detectable oxygen and moisture content to maintain inert processing chambers during wafer fabrication and packaging.
Requires high-pressure oxygen gas for partial oxidation and synthesis reactions, combined with continuous nitrogen streams for flare stack purging, vessel blanketing, and explosion prevention.
Demands massive volumes of gaseous oxygen for basic oxygen furnaces (BOF) and electric arc furnaces (EAF), alongside argon for secondary ladle refining and shielding.
Utilizes liquid nitrogen co-production for cryogenic flash freezing, controlled atmosphere packaging (CAP), and temperature-controlled bulk transit.
To assist our technical team in calculating precise cold box sizing, column diameter, compressor displacement, and power consumption for your site, project managers should provide the following baseline parameters:
Suzhou Fengyun Fluid Technology Co., Ltd. delivers full-lifecycle project support. Our engineering engagement extends well beyond equipment fabrication, encompassing civil engineering advisory, plant layout design, field piping installation, supervisory testing, and lifecycle operation and maintenance (O&M).
Our field deployment engineers coordinate foundation anchor placement, cold box vertical lifting, main air piping connections, vacuum-insulated pipe (VIP) installation, and cable tray routing in compliance with international industrial plant standards.
All skids undergo factory acceptance testing (FAT) including hydro-static pressure testing, electronic instrument loop checks, and helium mass spectrometer leak detection. On-site commissioning follows rigorous Site Acceptance Testing (SAT) protocol, verifying continuous purity stability, flow rating, and automated shutdown interlocks.
We offer flexible operational models—including turnkey gas sales, equipment leasing, and complete outsourced O&M. Our IoT smart control hub continuously monitors operating health, providing online fault analysis, energy consumption optimization, and rapid field dispatch.
We achieve ultra-high purity levels through precise multi-stage cryogenic fractional distillation columns combined with high-efficiency dual-bed molecular sieve purification systems. Moisture and CO2 are removed down to less than 1 ppm prior to cold box entry, preventing column fouling. Internal column internals utilize engineered structured packing to maximize liquid-gas contact area, enabling continuous separation of nitrogen, oxygen, and argon at exact boiling point differentials.
To calculate system sizing and energy performance, we require the desired flow rate for each gas product (Nm³/h), target purity levels, required delivery pressures at battery limit, local ambient temperature and altitude conditions, available utility power (voltage/frequency), and whether co-production of liquid gas is required for emergency backup storage.
All cryogenic pressure components operating at sub-zero temperatures are manufactured from high-grade cryogenic aluminum alloy (such as 6061-T6) or low-carbon austenitic stainless steel (SS304L/SS316L) to prevent low-temperature embrittlement. Cold box outer shells are fabricated from structural carbon steel filled with expanded perlite or vacuum powder insulation. All manufacturing complies with international pressure vessel design codes, supported by 100% NDT weld testing and helium leak checks.
Yes. Our air separation systems feature automated DCS/PLC load-following controls integrated with variable frequency drive (VFD) air compressors and automated guide vanes on turbo expanders. When downstream factory demand decreases, the system automatically turndowns compressor airflow and adjusts distillation column reflux ratios, maintaining product purity while minimizing electrical power consumption.
Suzhou Fengyun Fluid Technology provides complete turnkey support including engineering design, equipment manufacturing, site erection supervision, FAT/SAT testing, and operator training. Post-commissioning, clients can choose full O&M outsourcing, compressor leasing, or remote monitoring via our IoT smart O&M platform, which provides predictive alerts and 24/7 technical assistance to guarantee continuous production uptime.
edmondwong01@gmail.com
+86-13814563863
Room 101, Building 36, No. 399 Xiarong Street, Wujiang District, Suzhou,Jiangsu, China
* If you are interested, please leave a message on the left.
As professional cuztomized industrial cryogenic ASU solutions provider, Fengyun has built an IoT-enabled smart O&M platform that connects directly to your on-site equipment. It delivers proactive alerts, remote diagnostics and energy efficiency analytics, while dispatching local service teams for rapid response to keep your production running without interruption.
Quick Links