Custom Nitrogen & Oxygen Combined Air Separation Systems & Dual-Gas ASU Engineering Solutions
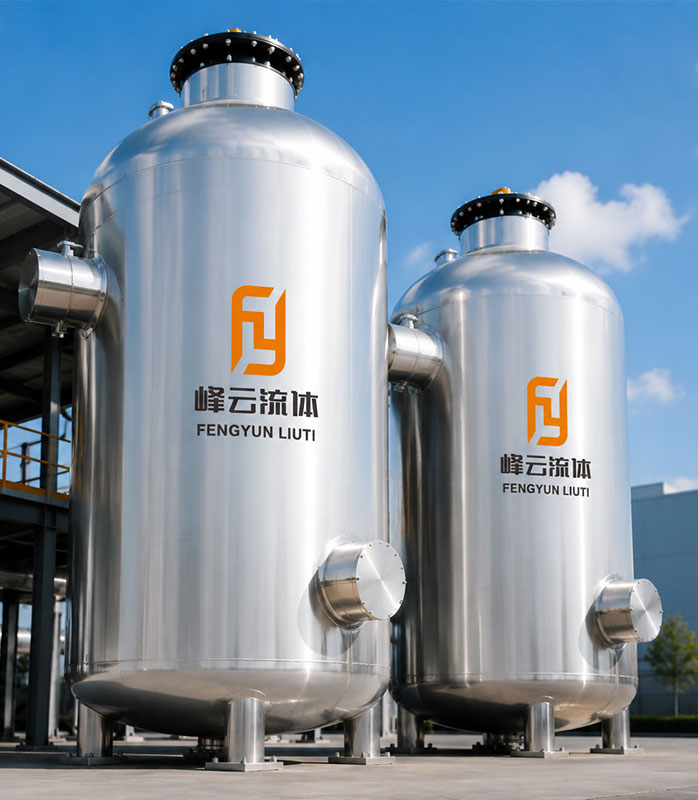
Suzhou Fengyun Fluid Technology Co., Ltd. is a premier engineering equipment manufacturer specializing in dual-gas and multi-gas cryogenic air separation units. Recognized among elite nitrogen oxygen combined air separation system manufacturers and leading China nitrogen & oxygen combined air separation system suppliers, we design, fabricate, erect, and commission custom air separation facilities that simultaneously extract high-purity gaseous nitrogen (GAN), gaseous oxygen (GOX), liquid nitrogen (LIN), liquid oxygen (LOX), and crude or refined liquid argon (LAR) from a unified atmospheric processing cold box.
Operating from our dedicated nitrogen & oxygen combined air separation system factory, our engineering team of 86 technical specialists integrates full-spectrum cryogenic separation infrastructures. By deploying optimized double-rectification columns, internal compression liquid oxygen/nitrogen pumps, brazed aluminum plate-fin heat exchangers, and energy-efficient expansion refrigeration turbines, our combined ASU systems eliminate the need for separate standalone oxygen and nitrogen plants. This unified process architecture lowers total capital expenditure (CAPEX), streamlines site footprint, and significantly reduces overall power consumption for multi-gas industrial complexes.
Direct Factory Engineering Value, Integrated Thermodynamics & Quality Standards
Partnering directly with a specialized nitrogen & oxygen combined cryogenic ASU plant factory provides project managers, EPC contractors, and plant engineers with complete technical transparency, direct factory pricing, and customized thermodynamic modeling. In multi-discipline manufacturing sites—such as integrated steelworks with chemical plants or glass works with annealing facilities—gas demand profiles require simultaneous continuous streams of oxygen for combustion or gasification and nitrogen for reactor blanketing, inerting, and purging.
At Suzhou Fengyun Fluid Technology Co., Ltd., we maintain total direct control over component fabrication and cold box integration. Our manufacturing facility executes precision welding, pressure vessel shell rolling, distillation column tray installation, and vacuum insulation fitting under strict ISO 9001, ASME Section VIII, and GB pressure equipment directives. Every combined ASU system undergoes rigorous non-destructive testing (NDT), X-ray weld examination, hydrostatic testing, and high-sensitivity helium mass spectrometer leak detection prior to factory dispatch, ensuring leak-free performance and decades of uninterrupted operation.
Unified Double-Column Fractional Separation
Our thermodynamic double-column cold box design extracts 99.6% pure oxygen and 99.999% (5N) pure nitrogen simultaneously from a single compressed feed air stream, maximizing ambient air yield and eliminating energy waste.
Internal Compression Dual Liquid Pumping
Utilizes submerged cryogenic pumps to pressurize liquid oxygen and liquid nitrogen inside the cold box before vaporization against booster air, delivering multi-pressure product gas streams to site pipelines without external gas boosters.
DCS Automation & Dynamic Ratio Tuning
Siemens DCS SCADA controls automatically rebalance column reflux ratios, compressor variable frequency drives (VFD), and turbo expander guide vanes, adjusting nitrogen-to-oxygen output ratios in response to shifting factory demand.
Selectable Combined Air Separation System Architectures & Product Series
To accommodate diverse gas consumption ratios, site utility constraints, and delivery pressure requirements, Suzhou Fengyun Fluid Technology presents a categorized suite of combined nitrogen and oxygen air separation plant configurations. Each series offers a configurable, field-proven engineering foundation:
Series 1: High-Oxygen Ratio Combined ASU Plants (Metallurgical Focus)
Optimized for integrated steelworks, non-ferrous smelters, and glass manufacturing hubs where gaseous oxygen demand dominates (60% to 80% of total gas output), while maintaining substantial gaseous nitrogen recovery for plant safety purging and ladle refining.
1. Integrated Steelwork High-Pressure Oxygen & Nitrogen Plant
Delivers continuous high-pressure oxygen gas for blast furnace enrichment and basic oxygen furnace blowing, while simultaneously supplying 99.999% pure gaseous nitrogen to bright annealing furnaces and site safety headers.
Technical Specs: Oxygen Capacity: 3,000 to 40,000 Nm3/h (99.6% purity); Nitrogen Capacity: 2,000 to 30,000 Nm3/h (99.999% purity); Oxygen Pressure: 0.8 to 3.5 MPa; Nitrogen Pressure: 0.6 to 1.6 MPa.
2. Oxy-Fuel Glass Furnace & Annealing Dual-Gas System
Supplies oxygen to oxy-fuel glass melting burners to increase thermal efficiency and reduce NOx emissions, while supplying pure nitrogen for tin bath atmosphere control in float glass production lines.
Technical Specs: Oxygen Purity: 99.5%; Nitrogen Purity: 99.999% (O2 ≤ 5 ppm); Integrated automatic liquid co-production ratio tuning.
Series 2: High-Nitrogen Ratio Combined ASU Plants (Petrochemical & Chemical Focus)
Designed for chemical synthesis complexes, coal gasification facilities, and petrochemical refineries where massive volumes of high-purity nitrogen are required for process blanketing, catalyst transfer, and flare stack purging alongside process oxygen.
1. Petrochemical Complex Nitrogen Inerting & Syngas Oxygen Plant
Supplies large-scale nitrogen gas pipelines for hydrocarbon storage tank blanketing and pipeline drying, while supplying high-pressure oxygen gas to partial oxidation gasifiers.
Technical Specs: Nitrogen Capacity: 5,000 to 50,000 Nm3/h (99.999% purity); Oxygen Capacity: 1,000 to 20,000 Nm3/h (99.6% purity); Fully automated trip safety interlocks.
2. Fertilizer & Ammonia Synthesis Combined Air Separation Unit
Extracts pure nitrogen feed gas for ammonia synthesis loops while generating high-purity oxygen for coal or heavy oil gasifiers, delivering complete atmospheric gas utilization for fertilizer plants.
Technical Specs: Nitrogen Purity: 99.999% (O2 ≤ 2 ppm); Oxygen Purity: 99.6%; High volumetric efficiency multi-stream plate-fin heat exchangers.
Series 3: Tri-Gas Full Fractionation Combined Plants (N2 / O2 / Liquid Argon)
Features advanced crude argon columns and packed deoxo distillation systems to recover high-purity refined liquid argon (LAR) alongside gaseous nitrogen and gaseous oxygen, delivering maximum commercial gas value.
Industrial Park Multi-Client Tri-Gas Combined ASU Complex
Engineered for centralized industrial parks to supply multiple tenant factories via pipeline networks with gaseous oxygen, gaseous nitrogen, and bulk liquid argon for precision welding, stainless steel refining, and solar ingot pulling.
Technical Specs: Oxygen Purity: 99.6%; Nitrogen Purity: 99.999%; Argon Purity: 99.999% (Ar ≥ 99.999%, N2 ≤ 3 ppm, O2 ≤ 1 ppm); Flow Scale: 10,000 to 60,000 Nm3/h.
Series 4: Modular Containerized & Skid-Mounted Combined ASU Units
Pre-assembled on rigid structural steel skids inside our specialized factory, these plug-and-play units reduce site civil works and simplify overseas shipping for remote mining camps, island sites, and modular refineries.
Modular Plug-and-Play Combined Oxygen & Nitrogen Generator Skid
Integrated air compressor skid, molecular sieve purifier skid, cold box module, and control panel array. Factory tested before dispatch for rapid site interconnection.
Technical Specs: Combined Flow Capacity: 500 to 3,000 Nm3/h; 85% pre-commissioned; Touchscreen operator HMI with remote cloud gateway.
Technical Specifications & Operating Parameters Matrix
The following practical specification matrix summarizes key performance thresholds, gas output purities, capacity scales, working pressures, and material selections across our primary combined air separation plant configurations:
| System Configuration |
Primary Target Products |
Achievable Gas Purities |
Combined Flow Capacity Range |
Battery Limit Pipeline Pressures |
Primary Structural Materials |
Automation & PLC Architecture |
| High-Oxygen Metallurgical Combined ASU |
GOX + GAN + LOX/LIN Buffer |
O2: 99.6%; N2: 99.999% (5N) |
5,000 to 50,000 Nm3/h |
O2: 0.8-3.5 MPa; N2: 0.6-1.6 MPa |
Austenitic SS316L / Al Alloy 6061-T6 |
Siemens S7-1500 PLC + WinCC SCADA / DCS |
| High-Nitrogen Chemical Combined ASU |
GAN + GOX + LIN Buffer |
N2: 99.999%; O2: 99.6% |
6,000 to 60,000 Nm3/h |
N2: 0.8-2.5 MPa; O2: 1.5-4.0 MPa |
SS304L / Brazed Al Heat Exchanger |
Redundant DCS + Safety Interlock Loop |
| Full Tri-Gas Fractionation ASU |
GOX + GAN + Refined Liquid Argon |
O2: 99.6%; N2: 5N; Ar: 99.999% |
10,000 to 60,000 Nm3/h |
Multi-stream pressure manifold |
Structured Al Packing / SS Cryo Valves |
Centralized Plant DCS + IoT Cloud Gateway |
| Merchant Liquid Dual ASU |
100% LOX + LIN + LAR Liquid |
High-Purity Bulk Liquid Grade |
100 to 1,000 tons/day liquid |
0.2 - 0.8 MPa storage filling |
Cryogenic SS Inner Tank / Carbon Steel Shell |
Automated Tank Farm Metering + Telemetry |
| Modular Combined Generator Skid |
GOX + GAN Skid Array |
O2: 99.5%; N2: 99.99% |
500 to 3,000 Nm3/h |
0.6 - 1.2 MPa |
Structural Carbon Steel Base / Al Cold Box |
Integrated Touch HMI + Remote Diagnostics |
Target Application Scenarios & Required Proposal Data
A combined oxygen and nitrogen air separation plant is the most economical engineering choice for multi-demand industrial facilities, maximizing compressed air thermodynamic utility while eliminating duplicate capital investment. As reputable manufacturers, we customize system designs for key industrial sectors:
Integrated Steel Metallurgy & Annealing
Provides oxygen for blast furnace enrichment and BOF converter blowing alongside pure nitrogen for stainless steel bright annealing furnaces and safety purging headers.
Petrochemical Refineries & Synthesis Complexes
Delivers high-pressure oxygen gas for partial oxidation gasification while supplying continuous high-volume nitrogen for hydrocarbon tank blanketing and pipe drying.
Float Glass Manufacturing & Oxy-Fuel Furnaces
Supplies oxygen for oxy-fuel melting burners to lower fuel costs and reduce NOx emissions while delivering pure nitrogen for protective atmosphere tin bath enclosures.
Multi-Client Industrial Park Pipeline Grids
Acts as a central utility anchor supplying neighboring tenant factories with customized pipeline oxygen and nitrogen streams under centralized metering.
Information Required for Custom Engineering Quotes
To enable our project engineering team to calculate thermodynamic mass-energy balances, size double distillation columns, and select optimal compressor frames, buyers should provide the following baseline parameters:
1. Product Gas Flow Rates: Required gaseous oxygen capacity (Nm3/h), gaseous nitrogen capacity (Nm3/h), and liquid co-production rates (tons/day).
2. Required Gas Purities: Oxygen purity percentage (99.5% or 99.8%) and nitrogen purity level (99.99% or 99.999%).
3. Battery Limit Delivery Pressures: Minimum required pipeline discharge pressure (MPa) for oxygen and nitrogen at the plant boundary.
4. Site Environmental Data: Ambient air temperature range, atmospheric pressure (altitude), relative humidity, and cooling water specifications.
5. Local Electric Power Utilities: Available high-voltage electric power parameters (e.g., 6kV/10kV, 50Hz/60Hz) and electricity tariff rate for specific power optimization modeling.
Turnkey Execution, Cold Box Erection, Acceptance Testing & Maintenance
Suzhou Fengyun Fluid Technology Co., Ltd. delivers full-lifecycle EPCM project support for combined air separation installations. Our experienced field engineers guide clients through civil layout design, equipment transport, cold box vertical lifting, perlite insulation filling, cold commissioning, and performance guarantee testing.
Field Cold Box Erection
Our installation specialists direct vertical cold box lifting, column precision alignment, vacuum insulation powder filling, and cryogenic pipe manifold welding to ensure complete structural integrity and zero thermal leakage.
FAT & SAT Testing Standards
Factory Acceptance Testing (FAT) validates vessel hydro-testing, valve stroke actuation, and PLC panel logic. Site Acceptance Testing (SAT) certifies plant cooldown timing, dual gas purity achievement, flow capacity, and emergency shutoff interlocks.
Lifecycle O&M & IoT Support
We offer flexible long-term maintenance agreements, spare parts stocking, compressor overhauls, molecular sieve re-bedding, and 24/7 cloud IoT diagnostic monitoring to ensure continuous plant uptime.
Frequently Asked Questions (FAQ)
1. What capital and operational cost benefits does a combined nitrogen and oxygen ASU offer over separate standalone plants?
A combined air separation plant utilizes a unified main air compressor, pre-cooling system, TSA molecular sieve purifier, and cold box structure. Compared to purchasing separate oxygen and nitrogen generators, a combined ASU reduces equipment capital expenditure (CAPEX) by 25% to 35%, lowers civil foundation footprint by up to 40%, and optimizes specific electrical power consumption (OPEX) by sharing refrigeration expansion cycles across both separation circuits.
2. How does the control system handle shifting factory demands when oxygen and nitrogen consumption ratios change dynamically?
Our automated Siemens DCS SCADA system incorporates advanced process control algorithms that interface with liquid compression pumps, air compressor VFDs, and expansion turbine guide vanes. When factory nitrogen demand increases while oxygen demand remains steady, the system automatically adjusts column liquid reflux ratios and expansion gas distribution, maintaining target purities for both product streams without wasting excess process air.
3. Can a combined nitrogen and oxygen air separation system also produce high-purity liquid argon?
Yes. In our Series 3 tri-gas combined plants, a side-arm crude argon distillation column and deoxo packing system are added to the main cold box. Because atmospheric air contains ~0.93% argon, extracting argon alongside oxygen and nitrogen captures additional high-value liquid product without increasing main feed air compressor energy consumption, maximizing overall plant profitability.
4. What safety features are engineered into the cold box to prevent hydrocarbon accumulation in liquid oxygen sumps?
Safety is paramount in cryogenic air separation. Feed air first passes through dual-bed TSA molecular sieve purifiers to eliminate acetylene and heavy hydrocarbons down to sub-ppm levels. Inside the main reboiler-condenser, liquid oxygen is continuously circulated and conditioned through secondary liquid phase adsorption beds. Furthermore, online total hydrocarbon (THC) gas chromatograph analyzers continuously monitor liquid oxygen sumps, triggering automatic purge procedures if hydrocarbon limits ever approach threshold levels.
5. What turnkey execution and long-term service support does Suzhou Fengyun Fluid Technology provide?
As a direct equipment engineering manufacturer, Suzhou Fengyun Fluid Technology provides complete turnkey project execution including plant design, equipment manufacturing, cold box vertical erection supervision, interconnecting piping, FAT/SAT acceptance testing, and operator training. Post-commissioning, clients benefit from 24/7 cloud IoT telemetry monitoring, predictive maintenance alerts, lifetime OEM spare parts supply, and long-term O&M service options.

 English
 中文简体