English
 中文简体
Call us
+86-13814563863

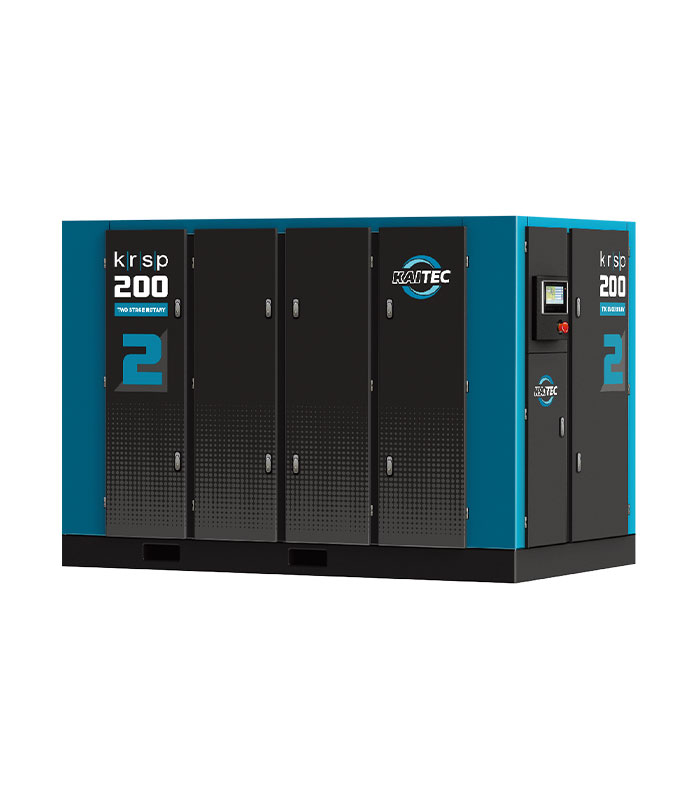

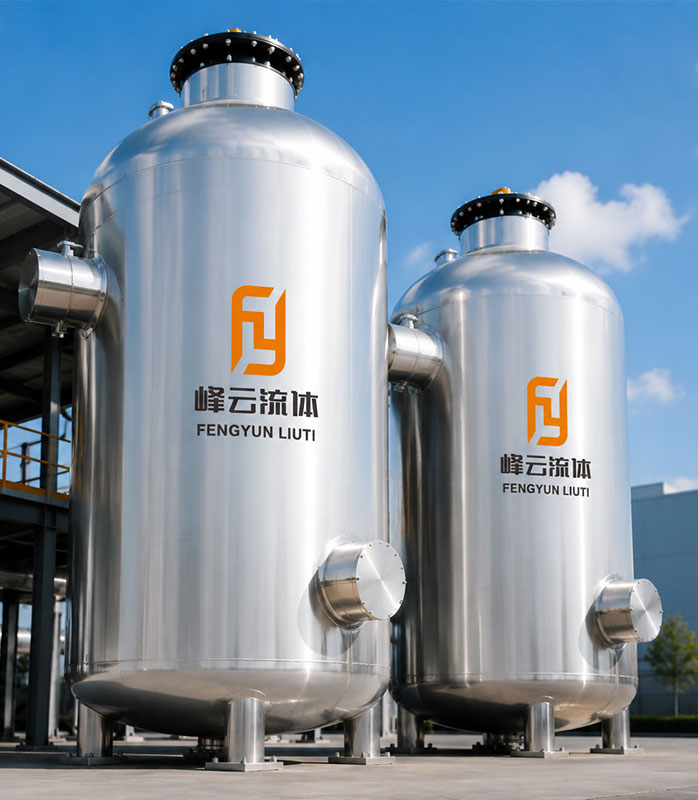
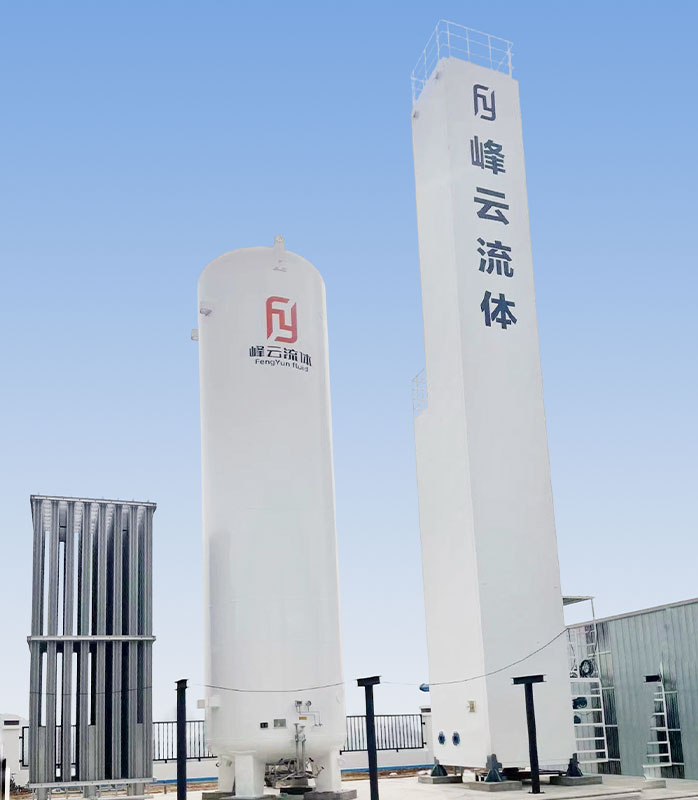
From on-site gas generation and gas recovery to air separation plant operation and maintenance, Fengyun Fluid provides full-lifecycle gas solutions for industrial clients.
Customer Value
Through advanced technology, intelligent management, and professional operational capabilities, we help our customers achieve:
1. Reliable Gas Supply
2. Cost Reduction
3. Enhanced Energy Efficiency
4. Green & Sustainable Development
Suzhou Fengyun Fluid Technology Co., Ltd. is famous China Cryogenic Air Separation Core Equipment Manufacturers and custom cryogenic air separation components suppliers, specializes in the design, manufacturing, delivery, and operation of cryogenic air separation systems for industrial oxygen, nitrogen, and argon.
Backed by a team of 86 engineers and technical specialists, the company's capabilities span air compression and separation station planning, air compression systems and air separation equipment sales and leasing, on-site gas generation, and outsourced technical services. Leveraging an IoT-enabled platform, Fengyun delivers smart gas supply solutions tailored to customer operations.
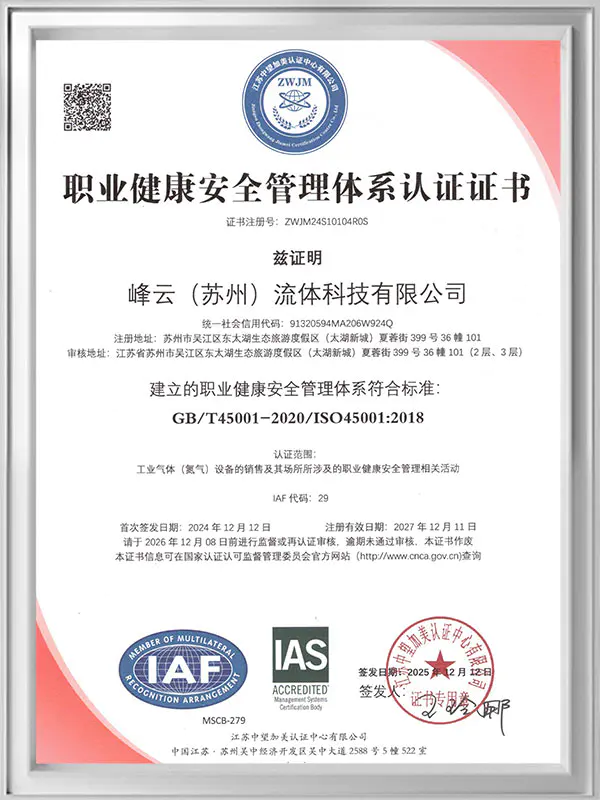
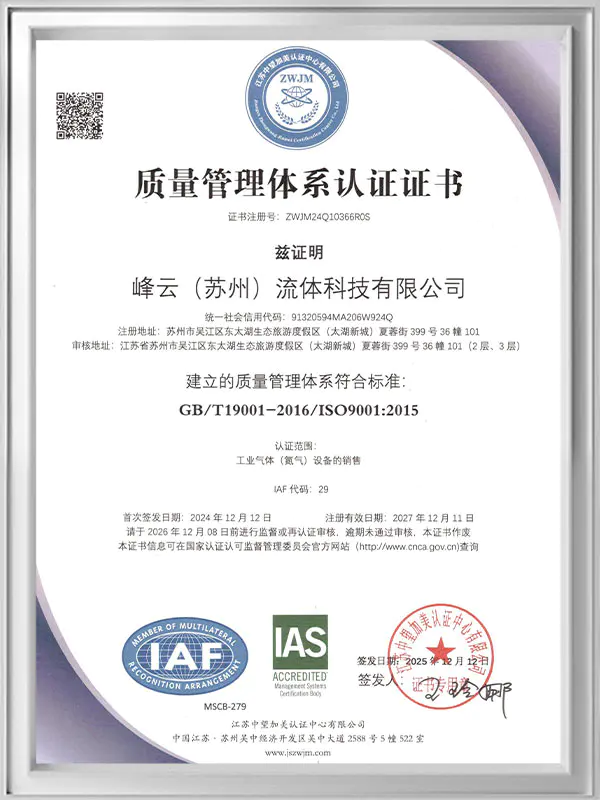
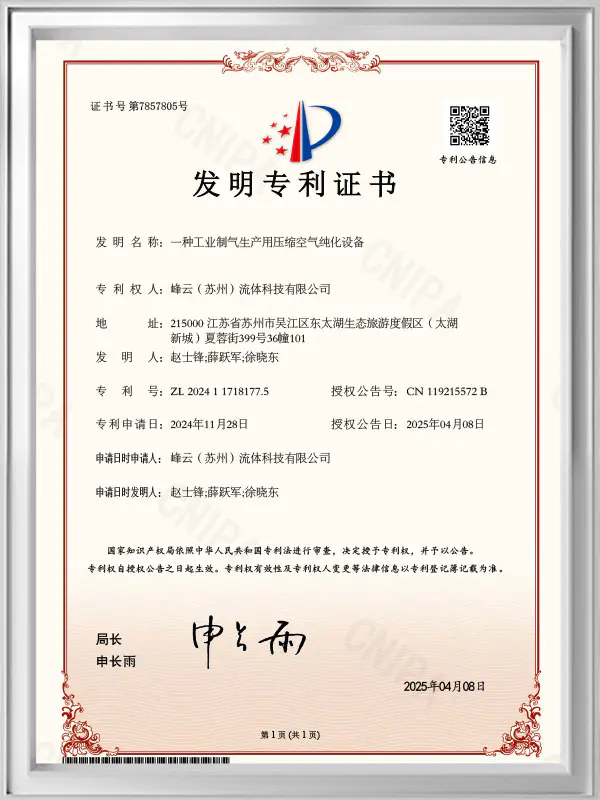
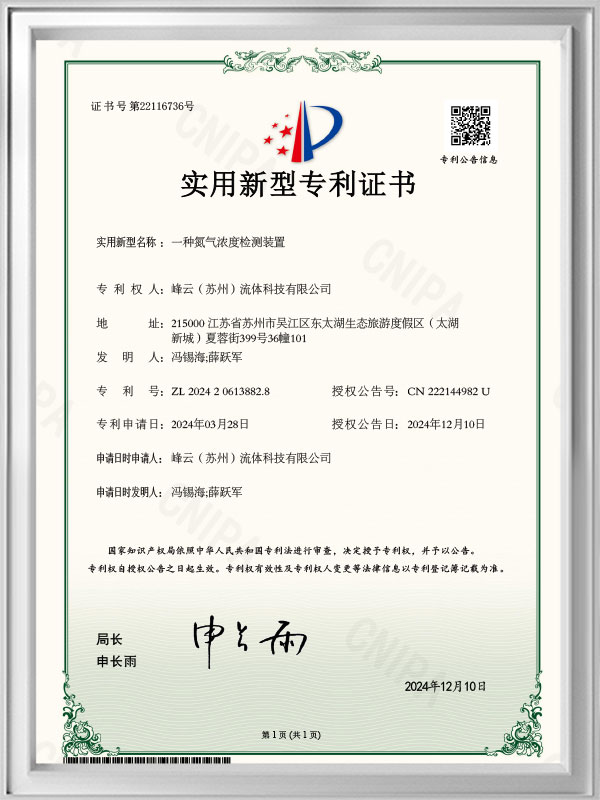
In large-scale industrial gas production, the Cryogenic Distillation Column (also referred to as the fractionation tower or distillation column) serves as the core thermodynamic separation unit. Oper...
READ MORENitrogen is an indispensable utility across modern manufacturing, chemical synthesis, metallurgy, and electronics fabrication. While smaller or medium-scale demands are frequently satisfied by Pressu...
READ MOREIndustrial gas supply is a critical backbone for modern manufacturing, energy, and chemical infrastructure. Among the various gas separation methods available today, the Cryogenic Air Separation Plan...
READ MORETraditional air separation plant operation relies heavily on on-site personnel, with slow fault response and high inspection costs. Fengyun Fluid integrates IoT technology into products and services, ...
READ MOREAt Suzhou Fengyun Fluid Technology Co., Ltd., we specialize in engineering and manufacturing high-precision core equipment and essential process machinery for cryogenic air separation units (ASUs). Recognized among leading China cryogenic air separation core equipment manufacturers, our company provides global gas producers, chemical plants, metallurgical complexes, and EPC contractors with custom-engineered mechanical components designed to operate under extreme thermodynamic conditions down to -196°C.
Our specialized technology product portfolio encompasses every critical subsystem required for efficient atmospheric gas separation. From heavy-duty rotary feed air compressors and temperature-swing molecular sieve purifiers to brazed aluminum plate-fin heat exchangers, high-purity distillation column cold box internals, precision turbo expanders, and submerged cryogenic liquid pumps, our machinery ensures superior power efficiency, zero atmospheric contamination, and decades of uninterrupted operational reliability.
Operating as a fully integrated cryogenic air separation components factory, Suzhou Fengyun Fluid Technology Co., Ltd. exercises full control over material selection, mechanical machining, specialized welding, vacuum assembly, and rigorous pressure testing. By manufacturing core machinery assets in-house rather than sourcing intermediate white-label parts, we provide technical decision-makers and plant engineers with complete component traceability, customized flange interfaces, and optimized thermodynamic matching across the entire separation circuit.
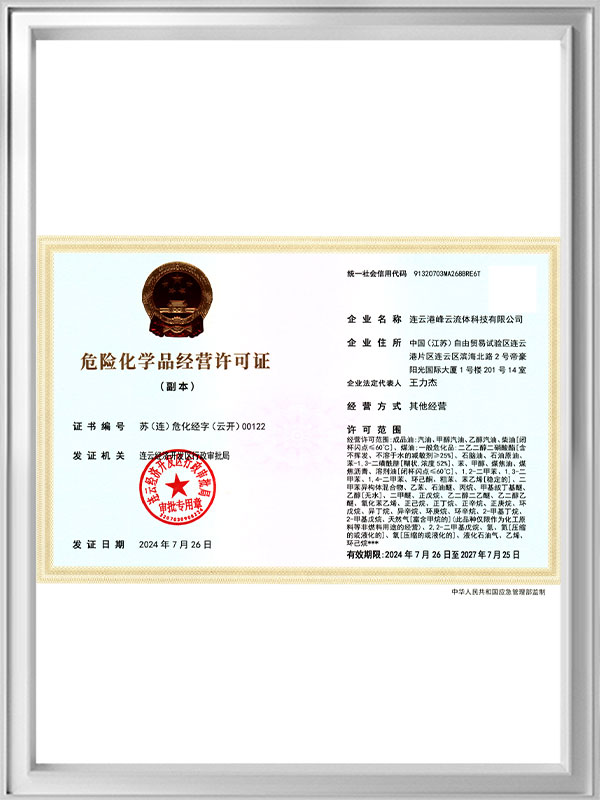
Our manufacturing facility adheres strictly to international pressure vessel and quality management frameworks, including ISO 9001, ASME Section VIII, and GB pressure equipment standards. Every structural casing, cryogenic piping manifold, and heat transfer matrix undergoes comprehensive non-destructive testing (NDT), X-ray weld examination, hydro-static testing, and high-sensitivity helium mass spectrometer leak detection before leaving our production bay.
All sub-zero pressure components are fabricated from certified cryogenic aluminum alloys (6061-T6, 5083) or low-carbon austenitic stainless steels (SS304L, SS316L) to prevent low-temperature ductile-to-brittle transition and ensure structural integrity under thermal shock.
Distillation column internals utilize structured aluminum packing and precision liquid distributors engineered via CFD fluid dynamics modeling, maximizing mass-transfer efficiency while drastically reducing column pressure drop.
Core machinery modules are equipped with integrated temperature sensors, differential pressure transmitters, vibration monitors, and automated control interfaces for seamless connection to main DCS and PLC supervisory networks.
To accommodate plant revamps, capacity expansions, or original system integration, Suzhou Fengyun Fluid Technology presents a complete range of specialized equipment modules. As trusted custom cryogenic air separation components suppliers, we engineer each subsystem to meet exact site conditions and operational duties:
The frontline process machinery responsible for drawing ambient air, elevating system pressure, cooling process gas, and eliminating atmospheric impurities before cold box entry.
Heavy-duty rotary screw and multi-stage centrifugal air compressors engineered for continuous 24/7 industrial duty. Model range KRSP-18-8 through KRSP2-455-10 delivers constant volumetric air flow at optimized discharge pressures.
Dual-vessel adsorption systems packed with high-capacity 13X synthetic zeolites and activated alumina. Automatically removes water vapor (H2O), carbon dioxide (CO2), and hydrocarbons from compressed feed air to prevent freezing blockages in sub-zero heat exchangers.
Core thermal transfer and fractionation equipment housed inside insulated cold box enclosures, performing deep refrigeration recovery and liquid-gas separation.
Multi-stream, compact heat exchangers constructed from vacuum-brazed corrugated aluminum fins and parting sheets. Achieves thermal effectiveness exceeding 98% between counter-current warming product gas streams and cooling feed air.
Upper and lower fractional distillation column assemblies manufactured from low-temperature aluminum alloys or austenitic stainless steel. Packed with corrugated sheet packing and precision liquid redistributors to isolate oxygen (99.8%), nitrogen (99.9999%), and crude/refined argon.
Rotating cryogenic machinery designed for refrigeration generation and high-pressure liquid transfer within internal compression cycles. Our specialized custom cryogenic air separation components factory manufactures dynamic rotating elements with extreme tolerance precision.
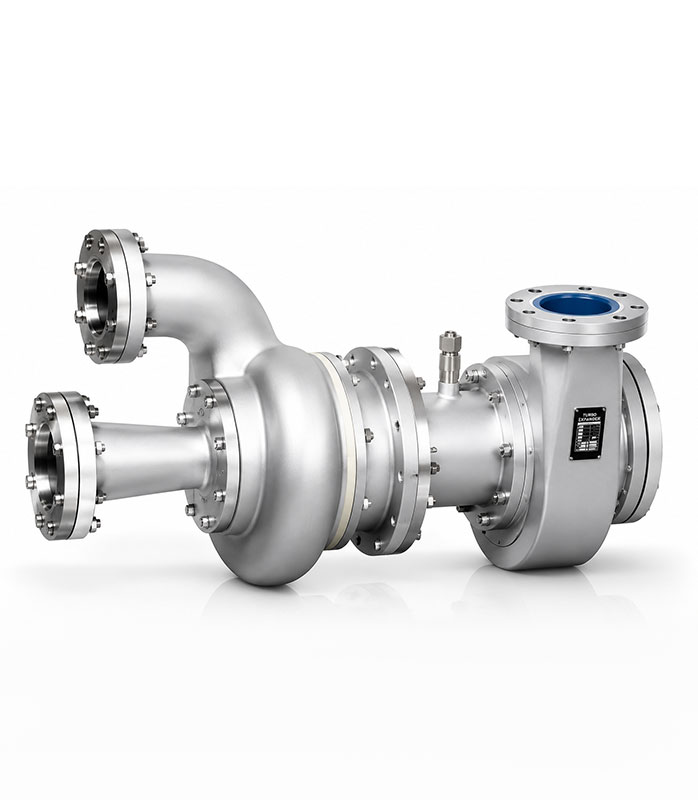
The primary refrigeration provider for the ASU. High-speed radial inflow turbines convert gas pressure enthalpy into mechanical work, producing refrigeration to maintain system thermal balance and drive air liquefaction.
Centrifugal and reciprocating cryogenic liquid pumps engineered for continuous operation in liquid oxygen, liquid nitrogen, and liquid argon service. Used in internal compression plants to pressurize cryogenic liquids prior to vaporization.
The following specification matrix provides a comparative technical summary across our key cryogenic machinery and core component lines:
| Equipment Category | Primary Duty & Function | Key Operating Parameters | Achievable Efficiency / Purity | Primary Construction Materials | Automation & Monitoring Interface |
| KRSP Air Compressor Station | Feed Air Compression | Power 18-455 kW; Press. 0.8-1.2 MPa | High volumetric screw efficiency | Ductile Iron / Alloy Steel Rotors | Integrated PLC / Modbus RS485 / VFD |
| TSA Molecular Sieve Unit | Feed Air Purification | Adsorption Press. 0.6-1.0 MPa | CO2 ≤ 1 ppm; H2O ≤ 1 ppm dew point | Pressure Vessel Steel Q345R / 13X Sieve | Automated Pneumatic Valve Switching PLC |
| Aluminum Heat Exchanger (BAHX) | Main Cold Recovery Heat Transfer | Operating Temp -196°C to +50°C | Thermal effectiveness ≥ 98% | Vacuum Brazed Aluminum Alloy 3003 | Multi-point Pt100 RTD Sensors |
| Distillation Column Vessel | Cryogenic Air Fractionation | Column Press. 0.15-0.6 MPa | O2 99.8%; N2 99.9999%; Ar 99.999% | Al 5083 / Austenitic SS304L | Differential Pressure Level Transmitters |
| Cryogenic Turbo Expander | Cold Box Refrigeration Expansion | Expansion Ratio 3.0 to 8.0 | Isentropic efficiency up to 88% | Forged Impellers / Gas Bearing Alloys | Automated IGV Control + Vibration Telemetry |
Our core cryogenic machinery and replacement modules are deployed across diverse industrial gas production environments, supporting new facility builds, revamps, and emergency plant repairs:
High-flow oxygen pumps, heavy-duty feed air compressors, and large-diameter distillation column modules designed for blast furnace enrichment and EAF steelmaking.
TSA purification skids and internal compression cryogenic liquid pumps tailored for coal gasification, ethylene oxide synthesis, and ammonia plant purge nitrogen supply.
Ultra-high purity nitrogen distillation internals, 6N purity analytical manifolds, and leak-tight stainless steel heat exchanger assemblies for electronics gas plants.
High-capacity liquefaction turbo expanders, liquid argon recovery columns, and bulk liquid nitrogen loading pump skids for merchant liquid suppliers.
To enable our engineering team to calculate thermodynamic heat exchanger balances, size expansion turbines, or design custom column interface flanges, please provide the following technical inputs:
Suzhou Fengyun Fluid Technology Co., Ltd. backs every core equipment component with comprehensive field engineering services. We assist plant engineers through installation oversight, alignment verification, pre-commissioning pressure tests, and long-term O&M maintenance.
Our technical specialists supervise cold box column positioning, plate-fin heat exchanger manifold welding, expander skid alignment, and perlite insulation packing to ensure zero mechanical strain and complete thermal isolation.
All core machinery undergoes strict Factory Acceptance Testing (FAT) including pneumatic pressure testing, dynamic balancing for turbo expanders, and helium leak detection. Site Acceptance Testing (SAT) verifies design flow rate, purity performance, and dynamic control stability.
We maintain an inventory of critical spare parts—including mechanical seal kits, expansion turbine wheel assemblies, and molecular sieve desiccant media—paired with 24/7 cloud IoT remote diagnostic monitoring.
Sourcing core equipment directly from our manufacturing facility ensures complete mechanical customization, strict quality control, and direct OEM engineering support without middleman markups. As specialized equipment builders, we manufacture distillation columns, molecular sieve beds, and heat exchangers in-house, ensuring complete thermodynamic compatibility and long-term spare parts availability for plant revamps and new ASU builds.
Brazed aluminum plate-fin heat exchangers offer up to 10 times the heat transfer surface area density per unit volume compared to shell-and-tube designs. They allow simultaneous multi-stream thermal exchange between warming product streams and cooling feed air with temperature approaches as close as 1°C to 2°C. This extreme thermal effectiveness significantly reduces energy consumption and cold box physical volume.
The temperature swing adsorption (TSA) molecular sieve unit removes moisture (H2O), carbon dioxide (CO2), and hydrocarbons (such as acetylene) down to sub-ppm concentrations. If unremoved, these compounds would freeze solid at cryogenic distillation temperatures (-180°C to -196°C), plugging heat exchanger passages, fouling column packing, and creating potential safety hazards in oxygen-rich liquid sumps.
Yes. Our 86-member engineering team routinely performs custom component retrofits and capacity expansions for existing cryogenic air separation plants. By analyzing site mechanical drawings and operating data, we manufacture custom-dimensioned distillation columns, replacement plate-fin heat exchanger cores, and upgraded molecular sieve skids that match existing cold box interface dimensions and piping flanges.
Every expansion turbine undergoes rigorous factory testing including high-speed dynamic balancing, hydraulic shaft bearing testing, static pressure housing tests, and full-speed run testing on compressed air test stands. We record vibration spectrums, bearing oil/gas temperatures, and aerodynamic nozzle response curves to guarantee flawless plug-and-play operation upon site installation.
edmondwong01@gmail.com
+86-13814563863
Room 101, Building 36, No. 399 Xiarong Street, Wujiang District, Suzhou,Jiangsu, China
* If you are interested, please leave a message on the left.
As professional cuztomized cryogenic air separation components factory, Fengyun has built an IoT-enabled smart O&M platform that connects directly to your on-site equipment. It delivers proactive alerts, remote diagnostics and energy efficiency analytics, while dispatching local service teams for rapid response to keep your production running without interruption.
Quick Links